
Industry Solutions
Automated Healthcare Storage
Discover automated storage solutions designed for temperature-controlled, regulated pharmaceutical and healthcare environments. Built to support GxP and MHRA requirements, our automated healthcare storage solutions keep regulated stock secure, traceable and easy to access while freeing valuable floor space.
Want to see how much stockroom you could recover? Speak to our team about automated pharmaceutical storage solutions, and we’ll conduct a free survey.
60%
Space savings
99.8%
Picking accuracy
100%
Audit compliance
<30s
Retrieval time
Industry Challenges
Common storage and logistics challenges across healthcare and pharmaceutical facilities:
- Temperature-controlled storage with limited floor space
- Strict regulatory compliance (GxP, MHRA)
- Full audit trail and traceability requirements
- Batch tracking and expiry date management
- Secure storage for controlled substances
- Cleanroom-compatible equipment needs
Healthcare operations rarely face these challenges in isolation. Space is limited, compliance requirements are increasing, and staff still need fast, accurate access to stock. Goods-to-person automation addresses all three by improving storage density, security and operational efficiency.
Our Automated Storage Solutions
Compact Lift
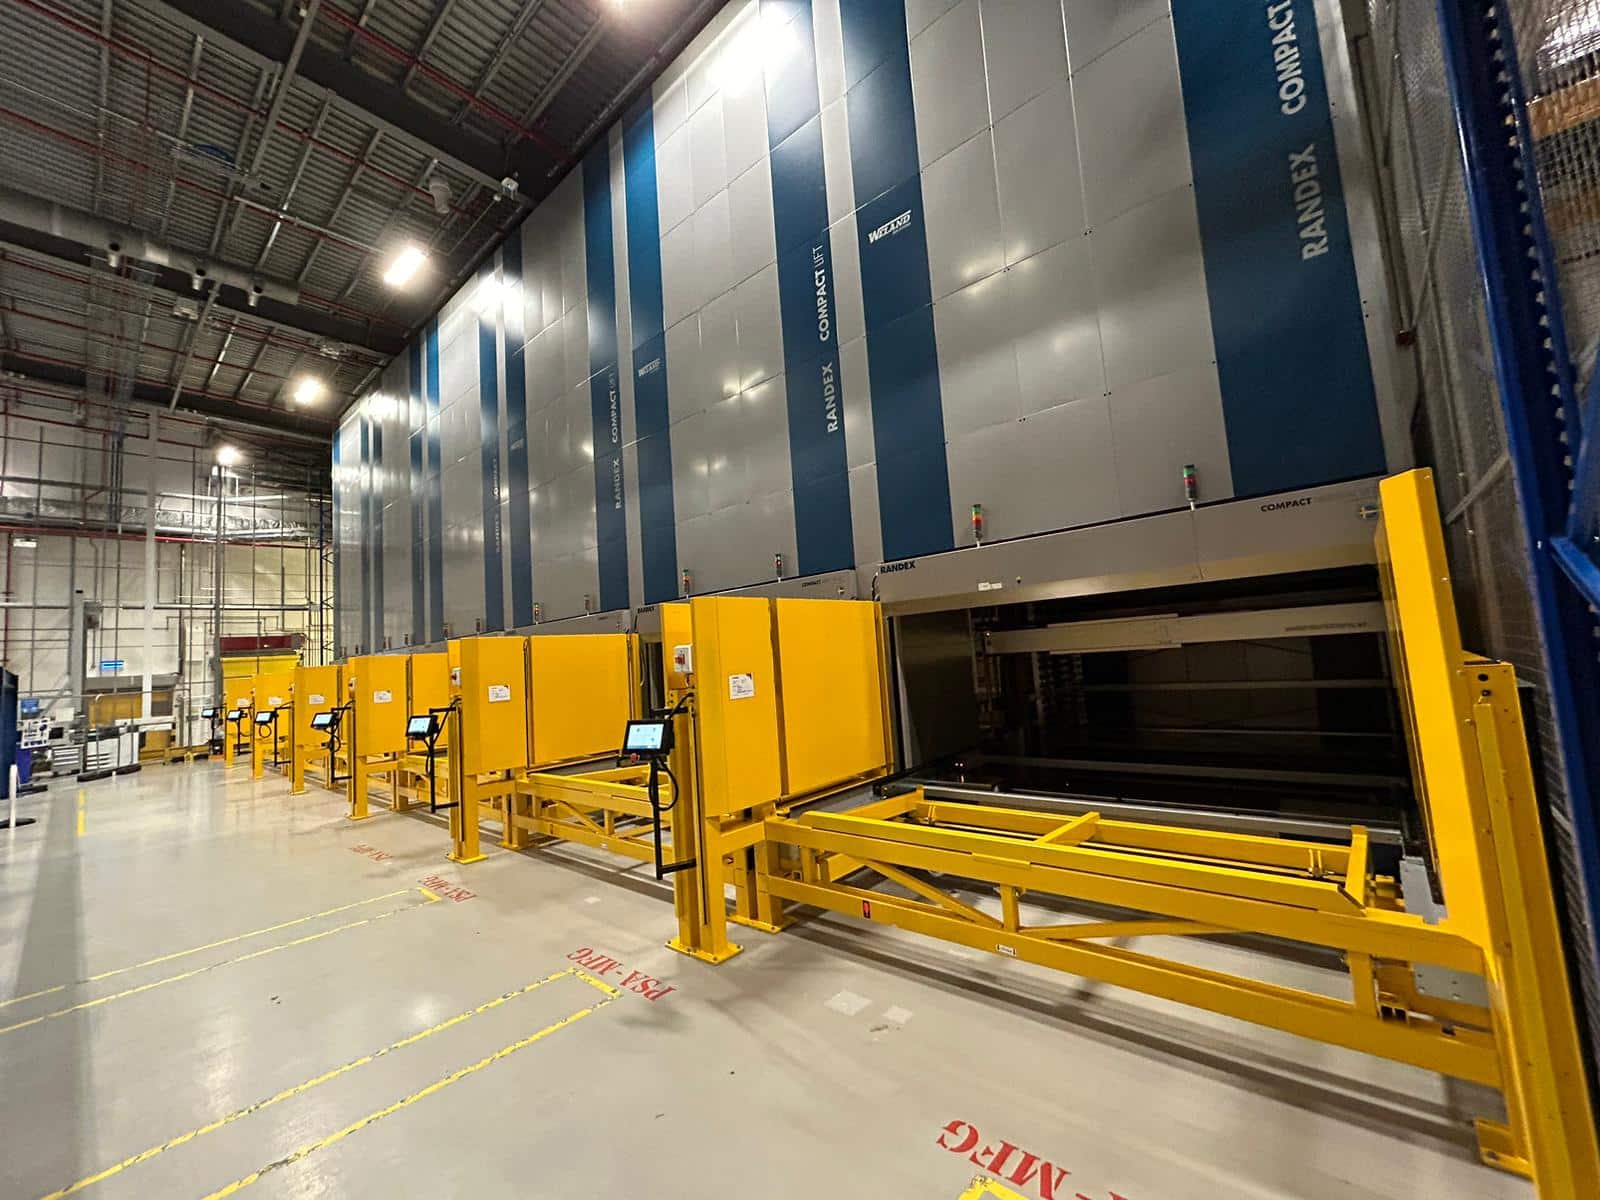
Temperature-controlled vertical storage with secure user access and full audit traceability, ideal for pharmaceutical warehouses and cleanrooms.
Learn more
Office Solutions
Secure document storage for regulatory files, clinical trial records and compliance documentation. Batch records stay indexed and lockable, keeping your paperwork organised, protected and ready for an inspection.
Learn more
Palomat
Stainless steel pallet dispensers meeting strict hygiene standards for pharmaceutical manufacturing. Empty pallets are stacked at floor level, so nobody is lifting them near a clean area.
Learn more
Automated Storage Systems for Regulated Stock
Vertical lift modules maximise storage capacity by using the full height of your building instead of expanding across the floor. Goods are automatically presented to the operator, reducing walking time while improving picking speed and accuracy. Compared with conventional shelving, automated storage systems free up to 90% of floor space while reducing search time and manual handling.
Precision drive technology positions every loaded tray accurately, allowing operators to complete up to four times as many picks, with less risk of human error.
Trays carry up to 1.5 tonnes, with a four-metre-wide modular option
The Compact Twin runs two trays at once, so picking carries on while the next arrives
Each machine is built to your building height rather than a fixed size
Automated inventory systems track items using unique serial numbers
How Automated Storage Compares With Manual Shelving
If you’re weighing up the switch, this is how the two approaches compare on the things a regulated stockroom is judged on.
| Manual Shelving | Automated Storage |
Floor Space | Spreads across the floor as stock grows | Uses the building height, freeing up to 90% of floor area |
Picking | Staff walk aisles and search shelves | Goods are presented to the operator, up to four times as many picks |
Errors | Depends on labels and memory | Software-directed picking reduces human error |
Access | Open to anyone in the room | Restricted by named permission, with a log of who opened it |
Audit Trail | Built by hand from paperwork | Recorded automatically as stock moves |
Manual Handling | Bending, stretching and lifting daily | Stock arrives at one window at working height |
Shelving still earns its place for bulky, slow-moving stock, which is why most sites run both. The table is about where each approach is strongest, not about replacing every shelf you own.
Medication Storage and Controlled Access
Not everything in a stockroom should be open to everyone. Under the Misuse of Drugs (Safe Custody) Regulations, certain controlled drugs have to be kept in a locked safe, cabinet or room. An enclosed machine with restricted access supports that, and the activity log shows you who opened it and when.
MHRA Good Distribution Practice also requires distributors to limit access to storage areas and to monitor the environmental conditions inside them. Where patient safety depends on the right item being picked, that control earns its place.

Inventory Management and Traceability
The machines integrate with leading warehouse management and inventory systems, providing real-time visibility of stock locations and movements.
Stock ranges from medications and medical devices through consumables. Sites store:
Boxed tablets
Vials
Dressings
Surgical instruments
Reagents
Batch numbers, expiry dates and inventory records remain in your existing software rather than in the machine. We integrate with the system you already run, so critical supplies stay where you expect them.
Bring us your stock list and we’ll provide a costed proposal showing how an automated system could work within your existing operations.

Proven in the Health Sector
Randex has supplied automated storage solutions to UK sites since 2004, and our client list includes Pfizer, Specsavers and the Ministry of Defence. We are the sole UK distributor for Compact Lift technology, built in Sweden by Weland Solutions.
That matters when you are choosing an automation partner, and so does their approach to your site. Healthcare providers want references in their own field, engineers who can reach them, and equipment that fits the way their operations already run.
FAQs About Automated Storage for Medical Supplies
Here is what stores and quality managers usually want to know before they specify a machine.
Can a vertical lift hold temperature-sensitive stock?
The machine is storage equipment rather than a refrigeration unit. It can be specified for a controlled environment and installed inside a temperature-controlled room, so your cold storage area works harder in the same footprint. We will confirm what your products are during the survey process.
Will one fit in a hospital pharmacy or a small stockroom?
Usually, yes. Machines are built to the height of your building rather than a standard size, so a tall narrow room suits them. A Compact Twin takes a footprint of roughly three metres by three metres and can hold around 200 square metres of storage. Hospital staff reach it from one window at a comfortable height.
How do we choose an automation partner for the healthcare sector?
Ask for references in the healthcare sector first, then look at what happens after installation. You want engineers who can get to you, a service contract in writing, and integration with the systems you already run. Proven expertise counts for more than a list of features when the stock supports patient care.
Can different temperature zones be accommodated?
Yes, by planning the zones first and placing a machine within each one. The equipment runs inside the controlled rooms you already maintain, so an ambient store and a cold room each get their own unit rather than one machine straddling both. We map your zones during the site survey and specify accordingly.
How much maintenance does the system require
A planned visit schedule keeps the machine in the condition it was commissioned in, and we run that from our own UK service operation. Contracts cover the visits, wear parts and remote diagnostics, with response levels up to 24/7 cover. You get the service record in writing, which your quality team will want for audits anyway.
Explore
Content & Resources
Case studies, articles and media from this industry sector.
Need a Storage Solution for Pharmaceutical & Healthcare?
Tell us what you store, how it must be controlled and who may touch it. We will design a system that helps you maximise space and optimise retrieval, and you will get a fully costed proposal.
We also supply automated pallet handling for bulk distribution, and vertical storage and retrieval systems for smaller parts.